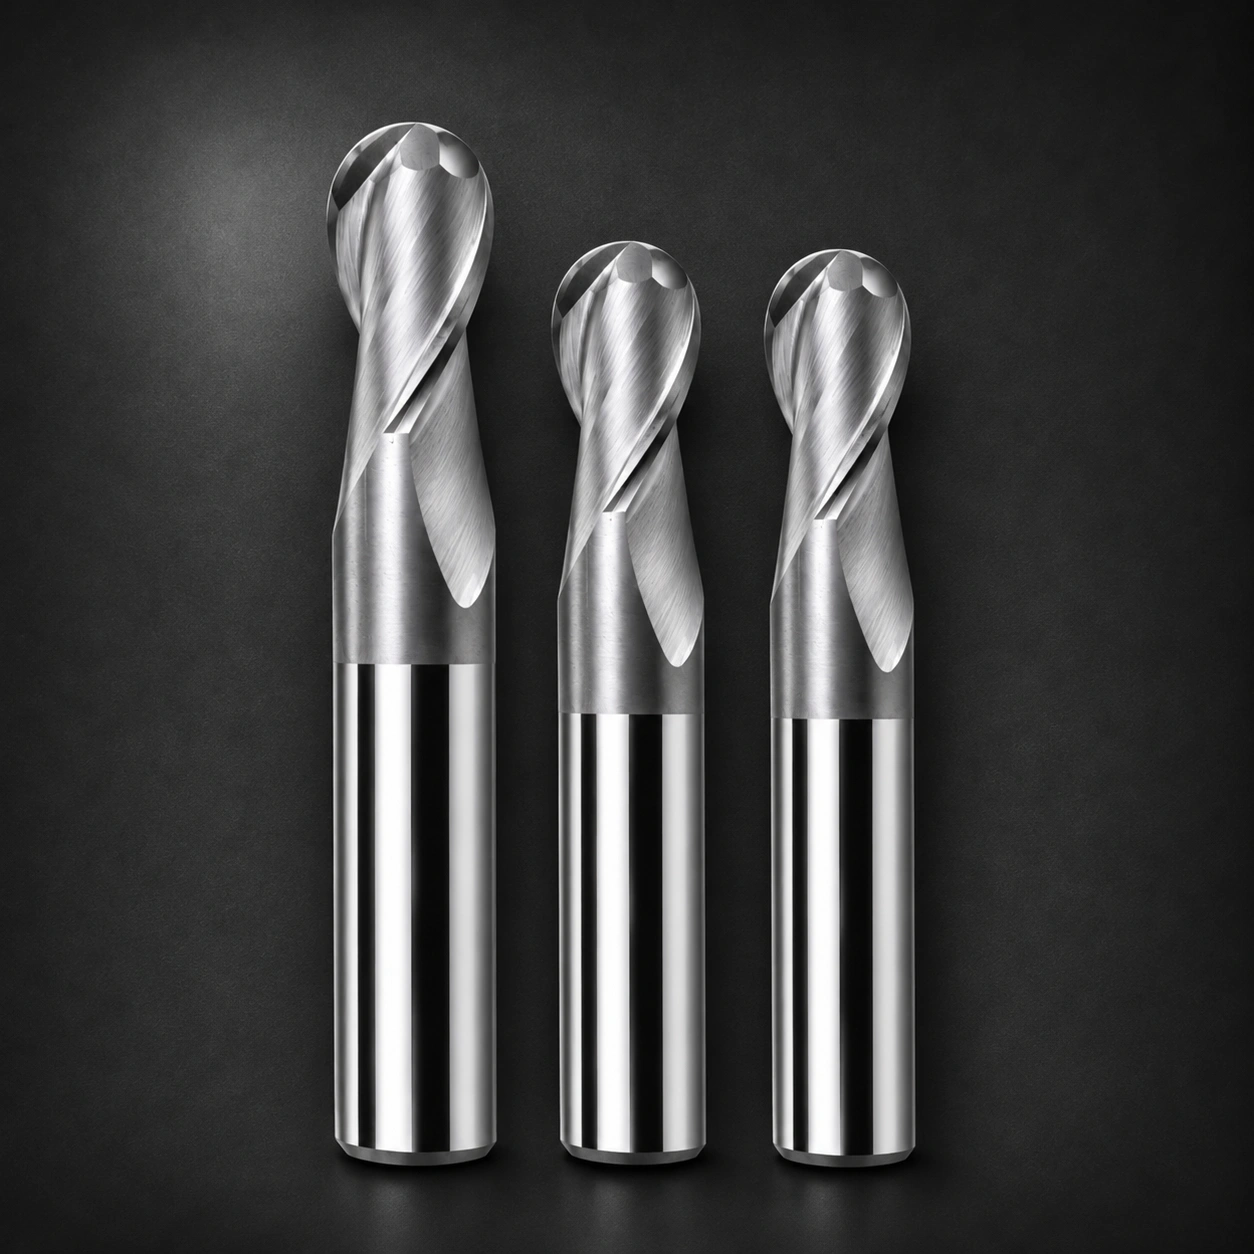
Description
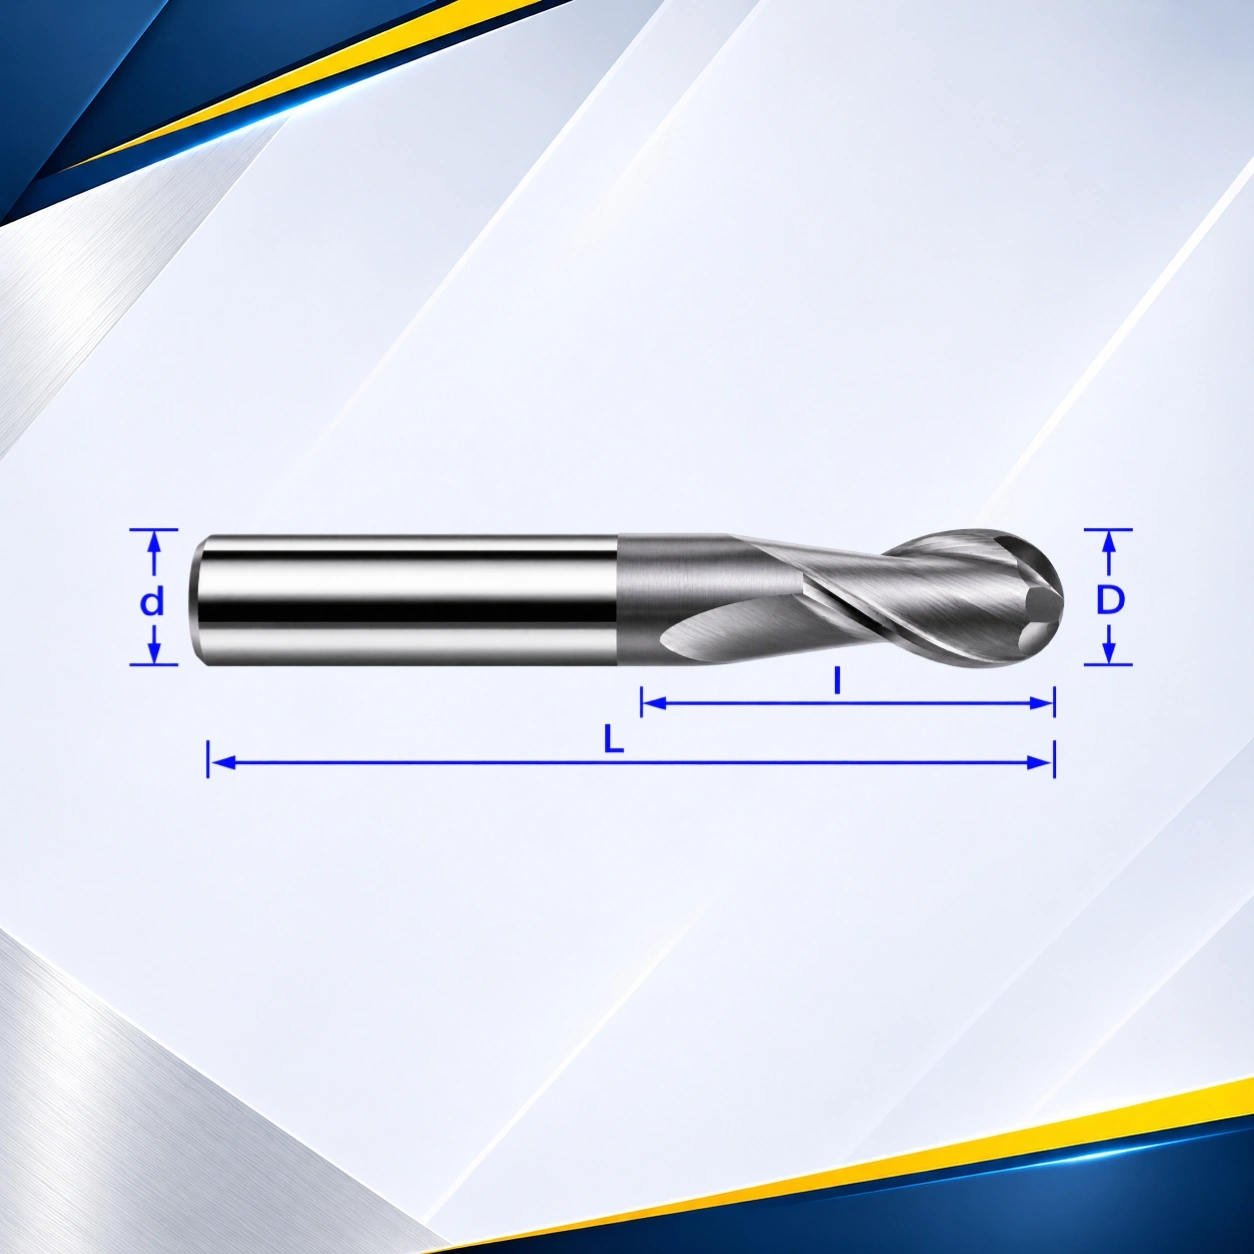
| CUTTING DIA MM (D) |
CUTTING LENGTH MM (L1) |
SHANK DIA MM (d) |
OVERALL LENGTH MM (L) |
NO OF FLUTE |
|---|---|---|---|---|
| 2 | 4 | 4 | 50 | 2 |
| 3 | 6 | 4 | 50 | 2 |
| 4 | 8 | 4 | 50 | 2 |
| 5 | 10 | 5 | 50 | 2 |
| 6 | 12 | 6 | 50 | 2 |
| 8 | 16 | 8 | 60 | 2 |
| 10 | 20 | 10 | 75 | 2 |
| 12 | 24 | 12 | 75 | 2 |
| 14 | 28 | 14 | 100 | 2 |
| 16 | 32 | 16 | 100 | 2 |
| 18 | 36 | 18 | 100 | 2 |
| 20 | 40 | 20 | 100 | 2 |
Application & Design
AlCrN Coating – Up to 50 HRC machiningSuitable for machining mold steel, welded parts, alloy materials, etc.
TiAlSiN Coating – Up to 60 HRC machiningSuitable for hardened mould steel, titanium alloy, Plastic mould & other difficult to machine materials.
Coating Type & Coating Colour & Coating Thickness
Coating Thickness
2–3 μm
2–3 μm
(Coating colours may vary. Colours shown in the illustrations are for reference purposes only.)